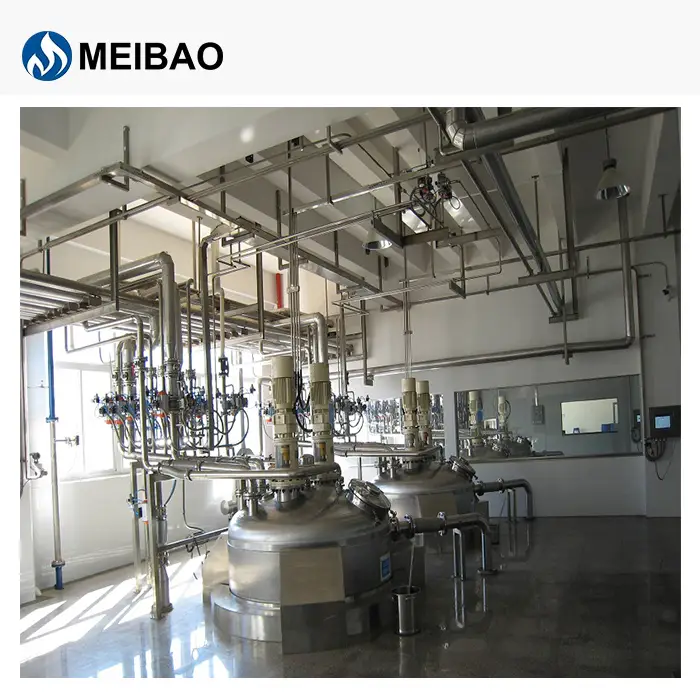
Waste and energy consumption are two of the biggest hidden costs in detergent manufacturing. They rarely appear prominently on a budget sheet, yet they quietly erode profit margins month after month. A plant that wastes raw materials, discards defective batches, or consumes excessive electricity is a plant that is losing money without even realizing it. MeiBao has designed their advanced liquid detergent production line specifically to address these hidden losses. By combining precision engineering with intelligent process control, their systems help manufacturers cut waste and reduce energy use in ways that deliver measurable financial returns. The environmental benefits are substantial, but the business case alone is compelling enough to warrant attention.
Precision Dosing Eliminates Raw Material Waste
The most direct way to reduce waste in detergent production is to stop wasting raw materials in the first place. MeiBao's automated dosing systems achieve this by measuring ingredients with extraordinary accuracy. Traditional manual dosing often results in over-pouring, spillage, and inconsistent measurements that lead to rejected batches. MeiBao's system eliminates these problems by dispensing exactly the required amount of each ingredient every time. The financial impact is significant, especially when dealing with expensive surfactants and fragrances. Over the course of a year, the savings on raw materials alone can be substantial. Beyond the cost savings, there is also the environmental benefit of reduced chemical consumption, which lowers the plant's overall ecological footprint.
Smart Mixing Reduces Energy Consumption
Mixing is one of the most energy-intensive stages of detergent production. Traditional mixers often run at full power for extended periods, consuming large amounts of electricity even when the mixture is already adequately blended. MeiBao's smart mixing technology changes this equation entirely. Their systems use sensors to monitor the state of the mixture in real time and adjust the mixer's speed and duration accordingly. Once the desired homogeneity is achieved, the mixer automatically reduces power or shuts off. This intelligent approach eliminates unnecessary energy consumption without compromising product quality. Over thousands of batches, the energy savings add up to a meaningful reduction in operating costs and carbon emissions.
Minimizing Product Loss During Changeovers
Changeovers between different products or batch sizes are notorious for generating waste. Product remaining in pipes and tanks must often be flushed out and discarded, and the first bottles filled after a changeover may not meet quality standards. MeiBao's production lines are designed to minimize these losses through features such as low-volume piping, efficient drainage systems, and rapid changeover procedures. The control system can also calculate the exact amount of product needed to purge the line, reducing the volume of wasted material. These design details may seem minor individually, but together they represent a significant reduction in waste over the course of a production year.

Reducing Rejected Batches Through Real-Time Quality Monitoring
A rejected batch is a total loss. All the raw materials, energy, and labor that went into producing it are wasted, and the batch must be disposed of responsibly. MeiBao's real-time quality monitoring systems help prevent this scenario by catching deviations before they become critical. Sensors continuously measure parameters such as pH, viscosity, and concentration. If a reading drifts outside the acceptable range, the system alerts the operator and can automatically adjust the process to bring it back on track. This early intervention capability dramatically reduces the likelihood of a batch being rejected, saving materials, energy, and time.
Energy-Efficient Components Throughout the System
MeiBao selects energy-efficient components for every part of their production lines. High-efficiency motors consume less electricity than standard alternatives while delivering the same performance. LED lighting in control panels and work areas reduces electricity consumption. Variable frequency drives on pumps and mixers allow them to operate at the optimal speed for each task rather than running at full power constantly. Even the control system is designed for energy efficiency, with standby modes that reduce power consumption during idle periods. These component-level improvements may seem small, but when multiplied across an entire production line running multiple shifts, the aggregate energy savings are impressive.
Water Conservation Through Recirculation and Reuse
Water is a critical resource in detergent manufacturing, used for cleaning, cooling, and as an ingredient. MeiBao's production lines incorporate water conservation features such as recirculation systems that allow cooling water to be reused rather than sent down the drain. Cleaning procedures are designed to use the minimum amount of water necessary, and wastewater is managed responsibly. In regions where water is scarce or expensive, these features provide both environmental and economic benefits. By reducing water consumption, MeiBao helps manufacturers operate more sustainably while also lowering their utility bills.
The Bottom Line: Efficiency That Pays for Itself
The combined effect of all these waste reduction and energy-saving features is a production line that costs less to operate and delivers higher profits. The initial investment in MeiBao's advanced technology is recovered over time through lower raw material costs, reduced energy bills, and fewer rejected batches. Manufacturers who have made the switch often report that the savings exceeded their expectations. In an industry where margins can be thin, these efficiencies provide a competitive advantage that is difficult to replicate. MeiBao's commitment to reducing waste and energy use is not just good for the planet; it is good for business, and that is a combination that makes sense for any manufacturer looking to thrive in the modern market.