Many commercial and industrial projects cannot be lit properly with off-the-shelf fixtures. Warehouses, cold stores, ports, factories, stadiums, and airports all have specific conditions, layouts, and regulations. Standard products may work for simple jobs, but complex sites often need lighting designed around their exact needs. That is where a capable led lighting manufacturer such as KML adds real value. Instead of adapting a project to fit catalog products, buyers get fixtures built for the job. This article explains why custom lighting works best with the right factory partner.
Why Choose a LED Lighting Manufacturer for Custom Solutions?
Custom lighting gives businesses more control over performance, quality, and long-term costs. When a factory designs fixtures around the actual space, energy use, and operating conditions, the result is better lighting and fewer compromises. Working directly with the producer also means clearer communication, expert guidance, and a more reliable supply. For contractors, developers, distributors, and facility managers, this approach turns lighting from a standard purchase into a carefully planned solution that supports the project’s goals from start to finish.
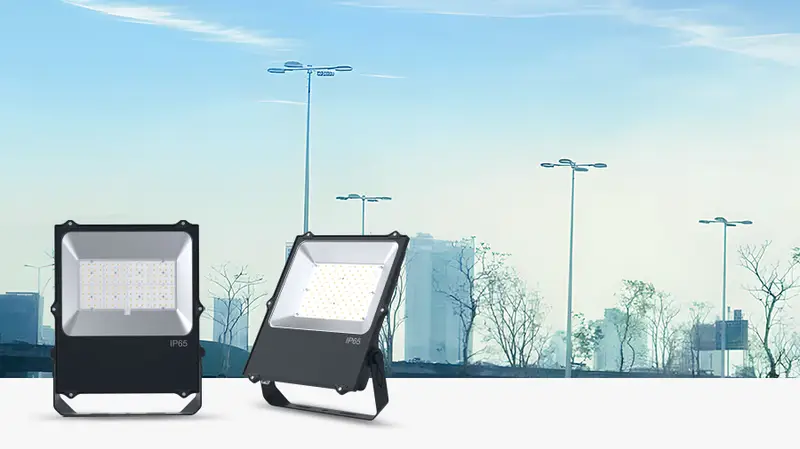
Access to Engineering Expertise
Factory engineers understand LED chips, driver stability, heat management, and light distribution in detail. This knowledge allows them to recommend the right setup for each project. A warehouse needs different brightness and beam angles than an office, store, or cold storage room. Engineers can adjust wattage, optics, and housing design to match ceiling height and working conditions. They also help buyers avoid common mistakes, such as choosing the wrong color temperature or insufficient output. KML’s dedicated team works on light distribution, heat dissipation, and intelligent control for exactly this purpose.
Fixtures Designed Around the Space
Every commercial building is different, with its own layout, ceiling height, environment, and usage. Custom lighting lets businesses get fixtures that suit their space rather than changing the space to fit standard lights. Factories can adjust materials, mounting methods, protection levels, and appearance. Outdoor fixtures may need stronger weather resistance, while factory lighting may need extra vibration resistance or high-temperature tolerance. KML, for example, has delivered customized cold storage lighting for a project in Hangzhou, showing how fixtures can be adapted to very specific conditions.
Tighter Quality Control
When buying through middlemen, it is hard to know how products were made or which components were used. Working directly with a factory gives buyers much better visibility. The factory controls material selection, assembly, and testing, which helps prevent defects and keeps performance consistent. This is critical for projects involving hundreds or thousands of fixtures. KML follows the ISO9001 quality system, inspects materials and products at every stage, and runs burn-in tests of eight hours or more before shipment.
Cost Efficiency on Large Orders
Many people assume custom lighting is always more expensive. In practice, working directly with a factory often costs less than buying through distributors, especially for large orders. Removing middlemen eliminates extra markups, and the factory can plan production around order volume. Custom fixtures can also reduce long-term costs, since they are designed to deliver exactly the right amount of light. This avoids over-lighting, lowers electricity bills, and may reduce the total number of fixtures needed for the project.
Stable Supply and Clear Schedules
Delays in lighting delivery can stall construction and increase labor costs. Working directly with a factory provides clearer information about production times, minimum order quantities, and shipping schedules. This makes project planning much easier. Regular customers often receive priority scheduling and smoother reordering. KML can deliver samples and small orders within about seven days and complete bulk orders within roughly 30 days, giving project teams realistic timelines they can plan around.
Private Label and Brand Differentiation
For distributors and wholesalers, offering something different from competitors is a major advantage. Working with a factory allows businesses to create their own branded products with custom logos, packaging, and features. This builds brand recognition and encourages repeat customers. Instead of selling the same generic lights as everyone else, distributors can develop product lines that match their brand and pricing strategy. KML’s contract manufacturing service supports this approach, including small-batch trial production and fast design changes.
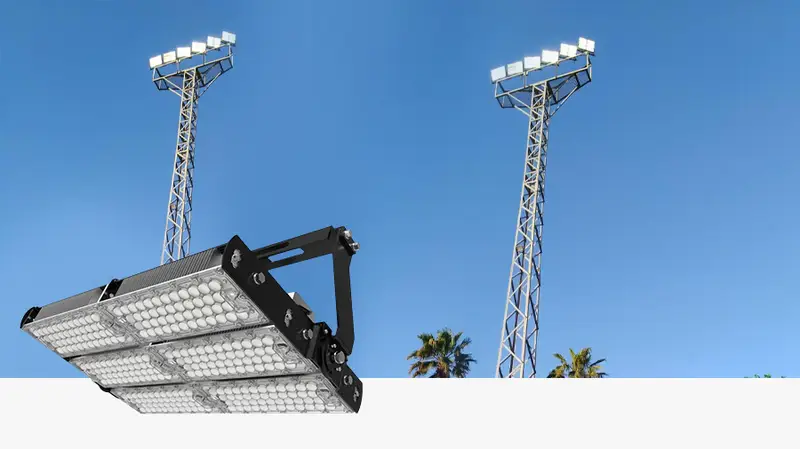
Compliance and Certification Support
Commercial lighting must meet safety and energy regulations that vary by country and industry. An experienced factory understands these rules and provides the required certificates and test reports. This is especially important for government projects and large corporate developments, where missing documents can delay approvals. KML lists CE, ETL, and CCC among the standards it supports, and its customization process allows certification requirements to be built into the project from the start rather than addressed later.
The Custom Process from Brief to Delivery
A well-organized custom process keeps projects on track. With KML, it typically begins with requirement discussions covering the application, environment, mounting height, brightness, color temperature, dimming, certifications, order volume, and lead time. The team then prepares a solution, often with simulation data within about 48 hours. Samples follow, allowing the buyer to test performance before mass production. Finally, products are packed with shock and moisture protection and shipped with full documentation. This structured approach turns complex lighting needs into reliable, finished installations.